

Elevator Pumps
In stock
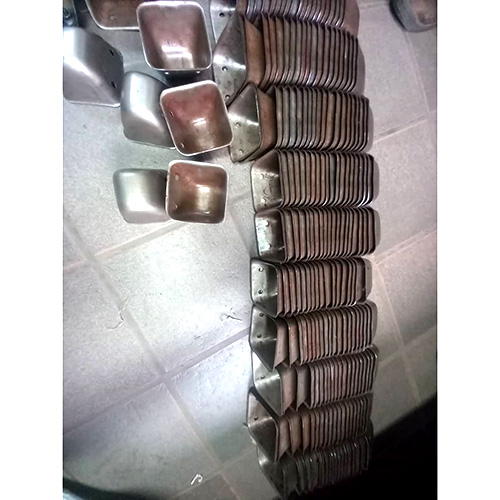
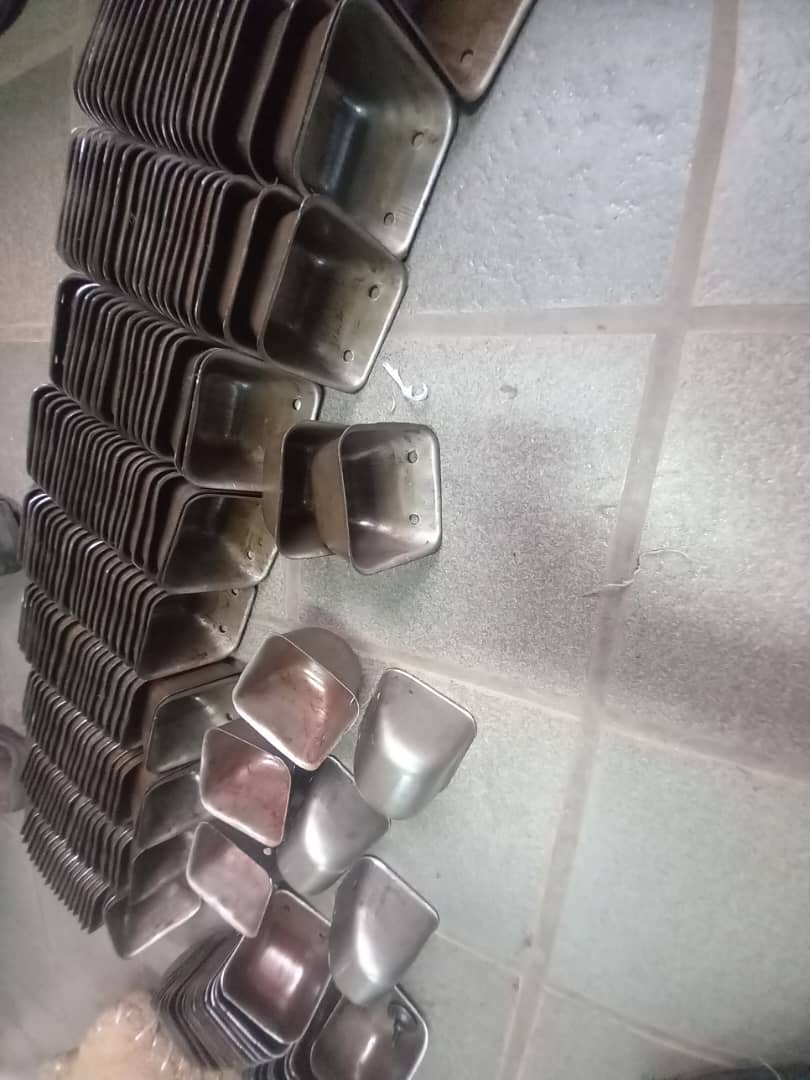
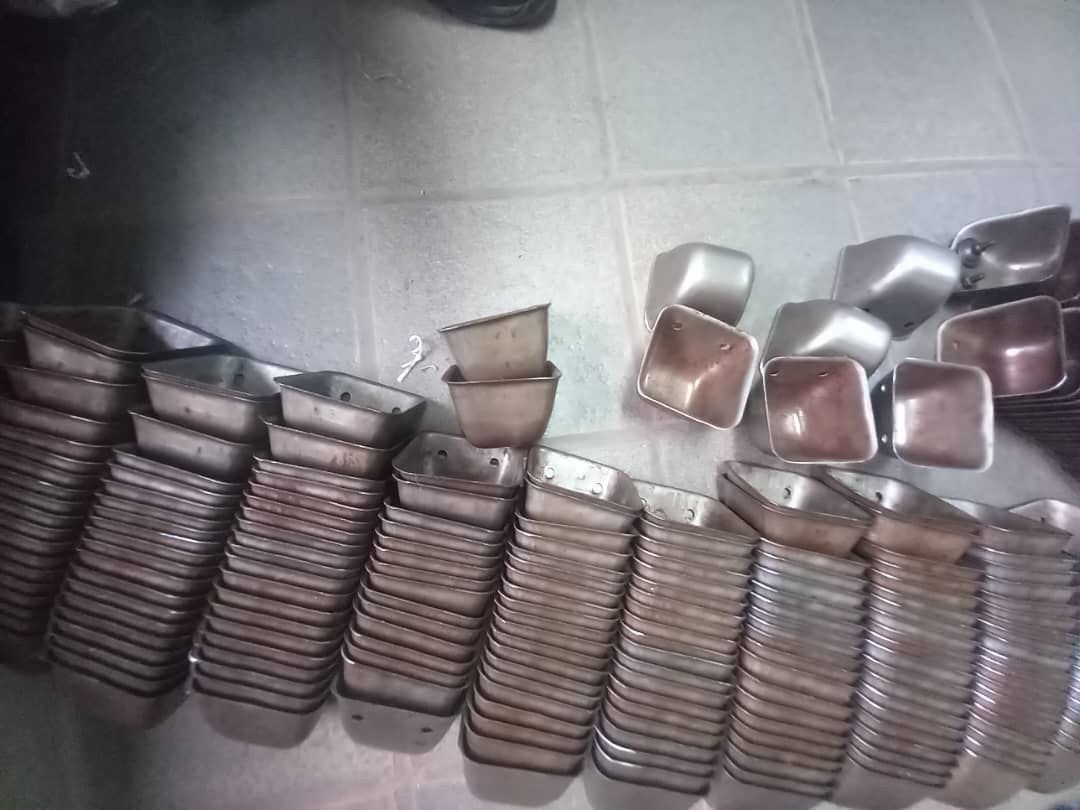
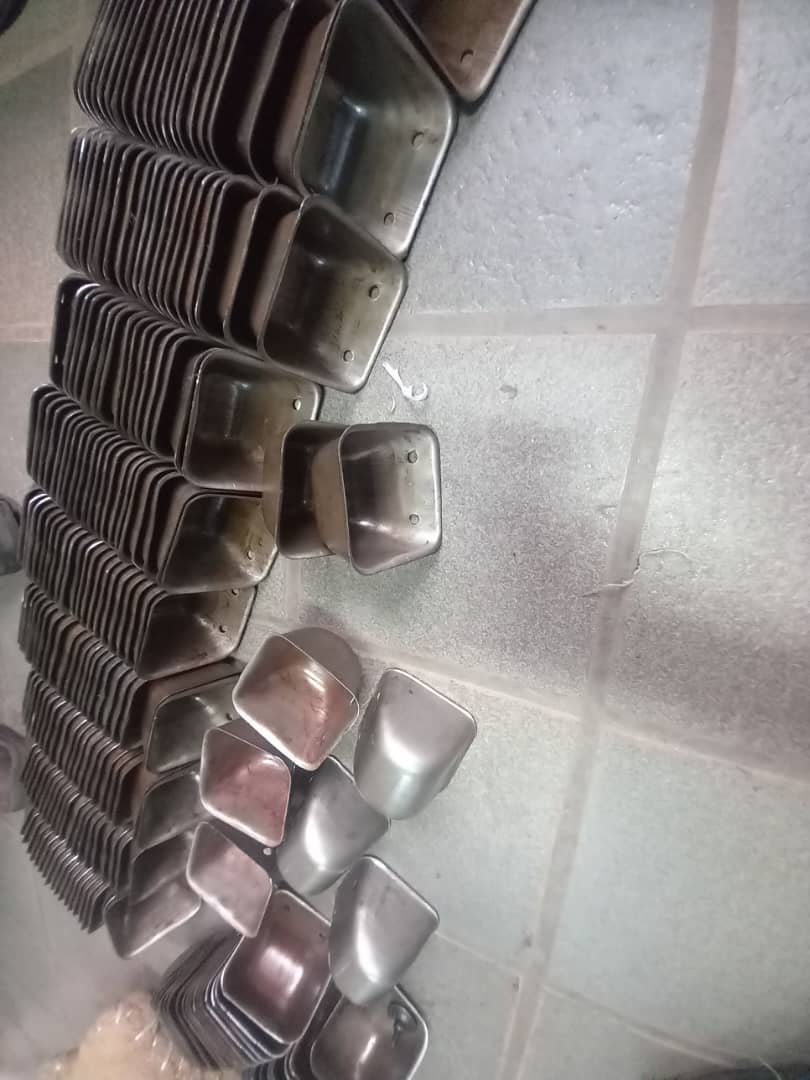
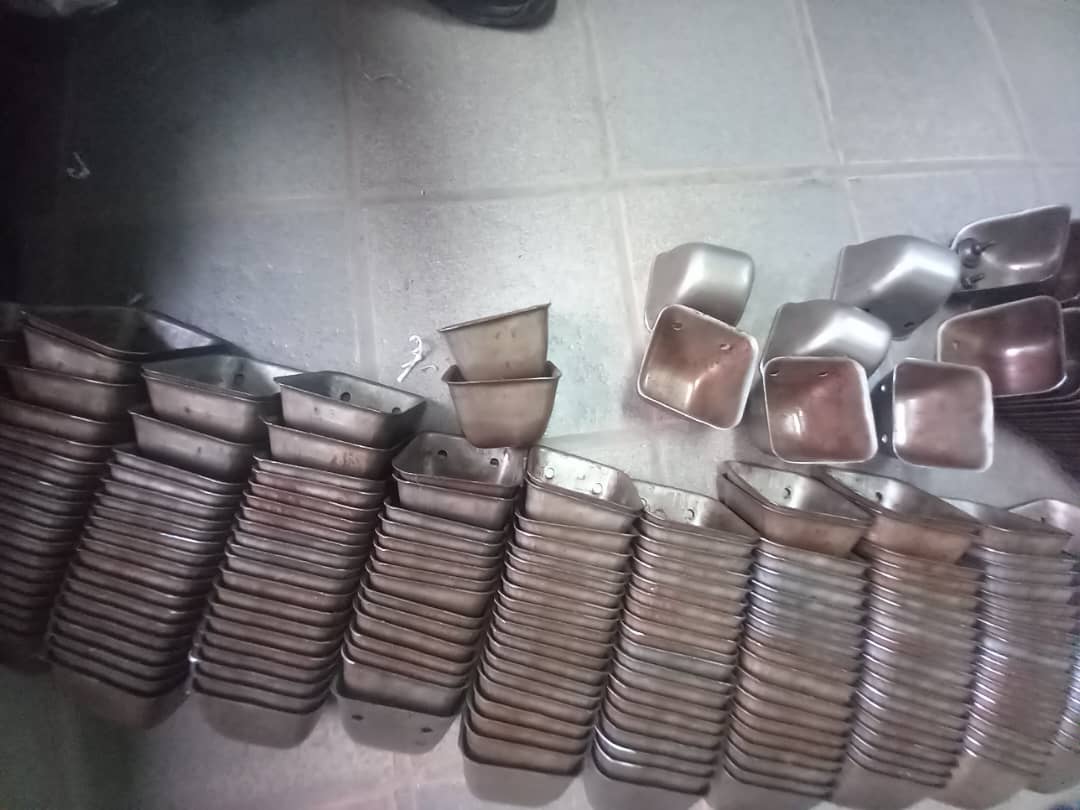
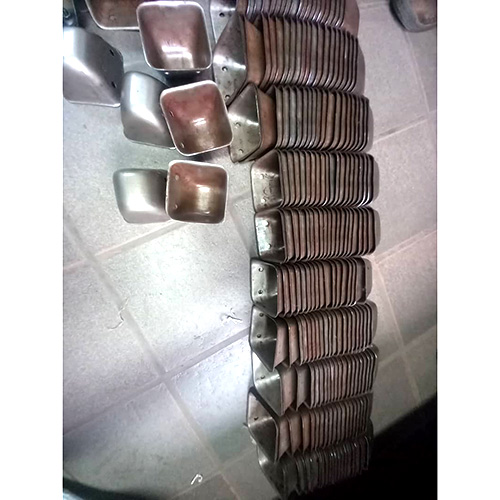
levator buckets are integral components of bucket elevators, designed to transport bulk materials vertically with ease and efficiency. Whether you’re handling grains, seeds, fertilizers, aggregates, or other free-flowing materials, our elevator buckets offer a robust solution for optimizing your material handling processes. With their superior design, durability, and performance, our elevator buckets ensure seamless and reliable operation in a wide range of industries.
- Superior Design for Optimal Performance: Our elevator buckets are meticulously engineered to deliver superior performance in material handling applications. The bucket shape, size, and profile are carefully designed to ensure efficient material discharge while minimizing spillage and product damage. With precision manufacturing and advanced materials, our buckets offer exceptional strength and wear resistance, enabling high-capacity vertical conveying while maintaining product integrity.
- Durable and Long-lasting Construction: We understand the demanding environments in which elevator buckets operate, and durability is a top priority. Our buckets are constructed using high-quality materials, such as food-grade polyethylene, nylon, or stainless steel, depending on your specific requirements. These materials provide excellent resistance to abrasion, corrosion, and impact, ensuring extended service life and minimizing downtime due to bucket replacement.
- Customization for Varied Applications: We recognize that different industries and materials have unique handling requirements. That’s why our elevator buckets are available in a range of sizes, shapes, and configurations to accommodate diverse applications. Whether you need shallow or deep buckets, wide or narrow, we can tailor the design to suit your specific material characteristics, capacity requirements, and installation constraints.
- Easy Installation and Maintenance: We believe that efficiency extends beyond performance, and that includes ease of installation and maintenance. Our elevator buckets are designed for hassle-free installation, featuring standardized dimensions and mounting options. Additionally, the smooth interior surfaces facilitate easy cleaning and minimize material build-up, reducing the risk of contamination and ensuring optimal hygiene in food and pharmaceutical applications.
- Enhanced Safety Features: Safety is paramount in any material handling operation. Our elevator buckets incorporate various safety features to protect personnel and equipment. Options such as low-profile design, non-sparking materials, and anti-static properties can be integrated to mitigate hazards associated with flammable or explosive materials, ensuring a safe working environment.
- Expert Support and Service: We pride ourselves not only on providing high-quality elevator buckets but also on delivering exceptional customer support and service. Our knowledgeable team is available to assist you in selecting the right bucket type and size for your application, as well as offering guidance on installation, maintenance, and troubleshooting. We are committed to your success and satisfaction throughout the lifecycle of your material handling system.
Invest in the efficiency and reliability of your material handling processes with our premium elevator buckets. Experience seamless vertical conveying, reduced downtime, and optimized productivity in your industry. Contact us today to discuss your specific requirements and explore how our elevator buckets can enhance your material handling operations.
Products

There are no reviews yet.